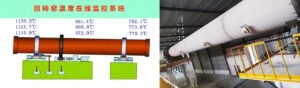
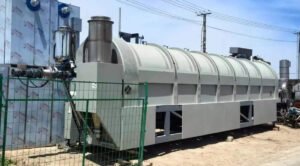
When a rotary kiln burner is operating normally yet fuel consumption remains high, the issue may stem from the preheater or cooler associated with the kiln.
If high-temperature flue gas fails to fully transfer its heat to the feed material, a significant amount of thermal energy is lost in the exhaust; similarly, if calcined products exit the kiln at excessively high temperatures and the cooler fails to promptly recover that heat, energy is wasted.
This not only increases fuel consumption per unit of product but can also complicate temperature control within the kiln.
In lime calcination, insufficient preheating increases the thermal load inside the rotary kiln; in cement clinker production, poor cooler performance can reduce heat recovery efficiency and destabilize secondary air, tertiary air, and combustion systems.
Therefore, simply raising the combustion temperature is usually not the optimal solution.
The correct approach is to treat the preheater, rotary kiln, and cooler as an integrated thermal system, comprehensively analyzing factors such as temperature, fuel, gas flow, material residence time, the degree of calcination, and heat losses.
What are rotary kiln preheaters and coolers?
Rotary kiln preheaters and coolers are located at the inlet and outlet ends of the thermal system, respectively. The preheater is responsible for “using waste heat to heat the feed,” while the cooler is responsible for “cooling high-temperature products and recovering heat.” They are critical pieces of equipment that influence the thermal efficiency of the entire calcination system.
The preheater utilizes high-temperature flue gas discharged from the rotary kiln to heat the raw materials entering the system, thereby reducing the amount of additional heat the materials need to absorb once they enter the kiln.
The cooler, meanwhile, cools the high-temperature calcined products exiting the rotary kiln and recovers as much residual heat from them as possible.
Therefore, although situated at different locations, both components impact:
Fuel consumption;
Thermal efficiency;
Temperature stability;
Degree of calcination;
Material residence time;
Product quality;
Fan power consumption;
Service life of refractory materials.
What is a rotary kiln preheater?
A rotary kiln preheater utilizes high-temperature exhaust gases from the kiln’s discharge end to pre-heat the raw materials before they enter the system. This means that once the materials enter the rotary kiln, they do not need to be heated from a low temperature; this saves a significant amount of fuel and makes it easier to control the temperature inside the kiln.
There are various types of preheaters—such as vertical preheaters, multi-stage suspension preheaters, and grate preheaters—and the specific choice depends primarily on the material characteristics and the production process.
Its main functions are to recover waste heat from the kiln exhaust, raise the temperature of the feed material, and reduce the heating load on the rotary kiln, all while stabilizing the operation of the entire thermal system.
For example, in lime production, limestone first passes through a preheater where hot exhaust gases raise its temperature before it enters the rotary kiln for calcination.
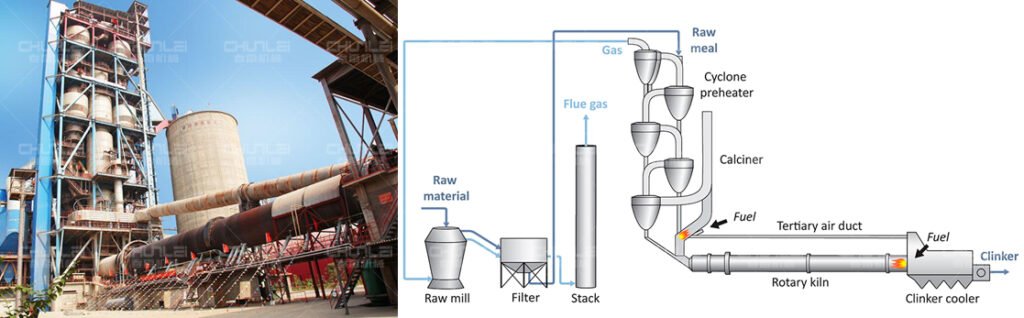
Cement production is more complex; raw materials undergo multi-stage preheating, and some systems include a calciner, allowing many decarbonation reactions to be completed before the material even enters the rotary kiln.
Therefore, when selecting equipment or managing operations, one cannot simply apply a standard temperature or calcination rate across different preheaters; decisions must be based on the specific process and materials involved.
What is a rotary kiln cooler?
Simply put, a rotary kiln cooler is a device used to lower the temperature of the hot product discharged from a rotary kiln.
Common types include rotary coolers, grate coolers, and planetary coolers, alongside other cooling equipment customized for specific processes.
However, a cooler does more than just “cool down the product.” What truly matters is recovering and utilizing as much of the product’s heat as possible while the cooling process takes place.
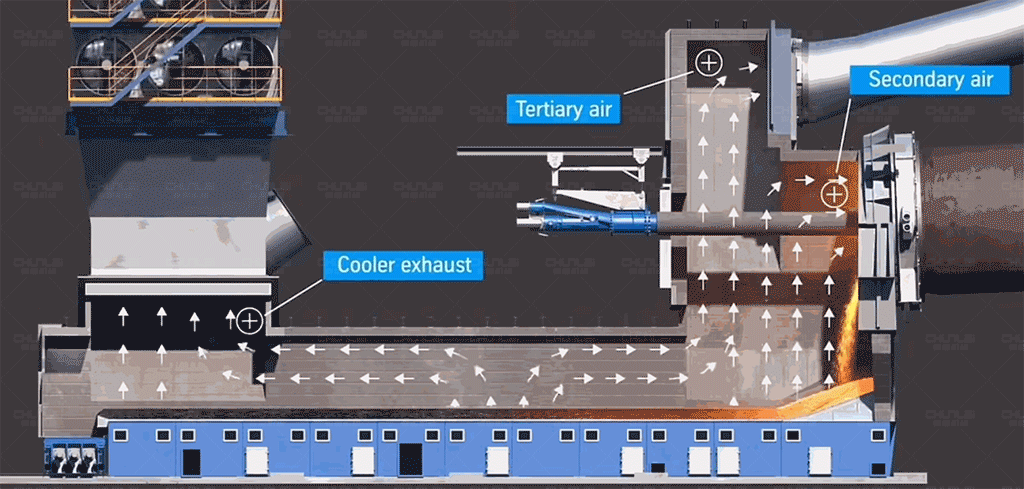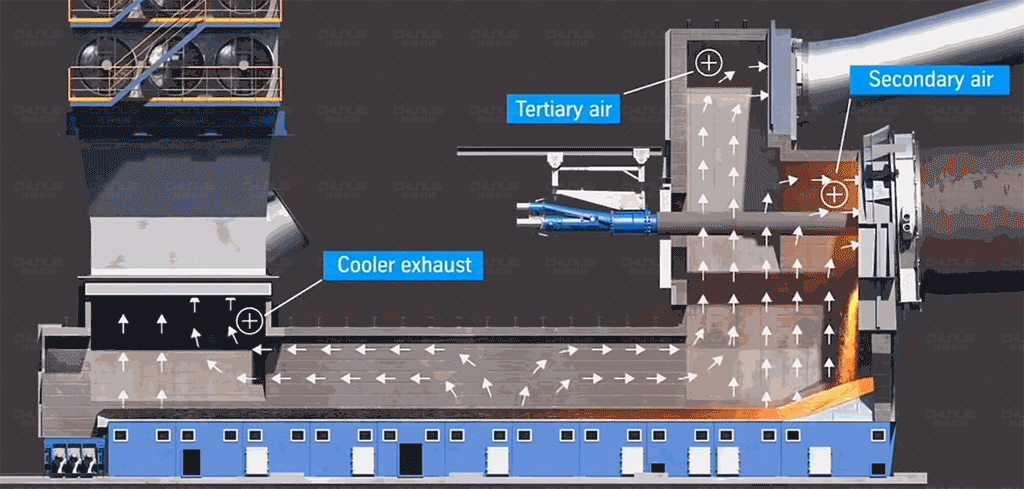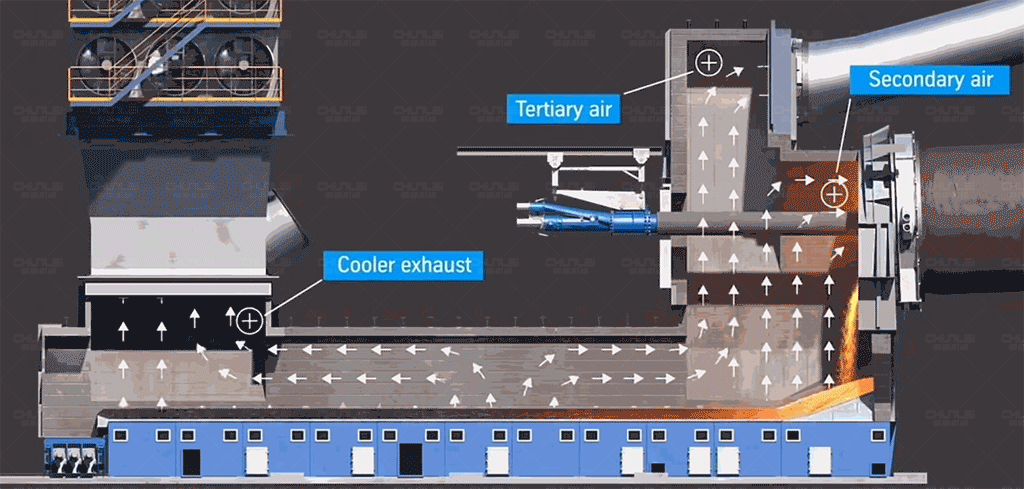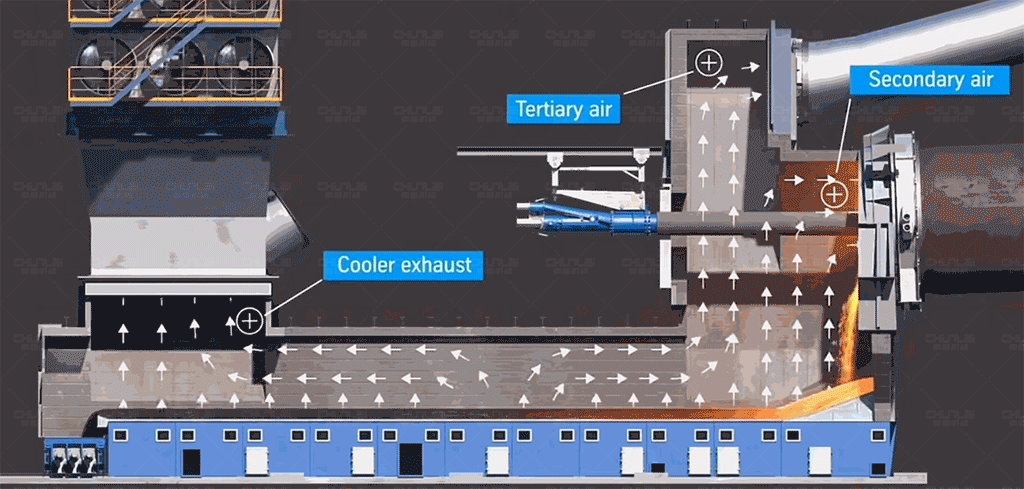
In cement clinker production, for instance, a grate cooler is used to cool the clinker; the hot air carrying the recovered heat is then fed back into the rotary kiln or calciner to serve as secondary or tertiary air, thereby minimizing heat loss.
The same applies to lime production: the primary goal is to cool the high-temperature lime to a suitable level while—where feasible—recovering the sensible heat to boost the system’s overall thermal efficiency.
How do the preheater, rotary kiln, and cooler work together?
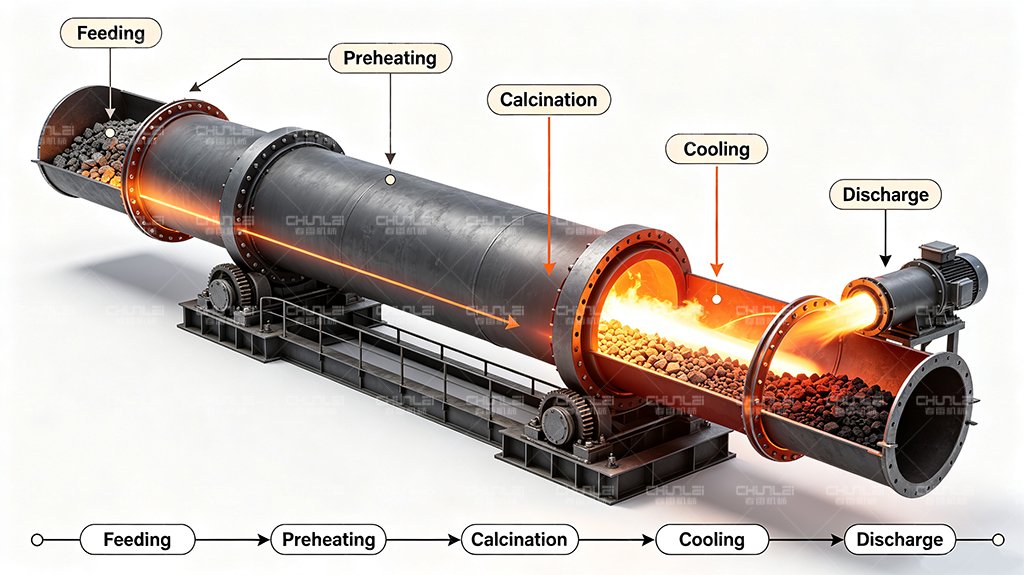
The entire thermal process can be simply represented as: Preheater → Rotary Kiln → Cooler
Process Stage
Main Inputs
Core Function
Main Outputs
Key Indicators
Preheater
Raw material + High-temperature flue gas
Recover flue gas heat and preheat material
Heated material + Cooled flue gas
Material outlet temperature, flue gas temperature, pressure drop
Rotary Kiln
Preheated material + Combustion heat
Complete primary thermal reactions
High-temperature calcined product
Temperature profile, residence time, calcination degree
Cooler
High-temperature product + Cooling air
Cool product and recover heat
Cooled product + Heated air
Product outlet temperature, recovered air temperature
These three components cannot be analyzed in complete isolation. For example, increasing the heat recovery efficiency of the cooler may raise the temperature of the secondary air entering the rotary kiln, thereby reducing the additional energy required to heat the combustion air. However, the ultimate outcome also depends on:
fuel properties;
burner performance;
air volume;
oxygen concentration;
material properties;
rotary kiln temperature;
product quality requirements.
How does a rotary kiln preheater work?
Simply put, a rotary kiln preheater uses the high-temperature exhaust gas from the kiln’s discharge end to preheat the raw materials before they enter the kiln itself.
What are the benefits of this? The higher the temperature of the material upon entering the kiln, the less heat the kiln needs to consume, resulting in higher production efficiency.
The working process is actually quite straightforward:
Material enters the preheater: Materials such as limestone or cement raw meal are fed into the preheating system.
Heating via high-temperature exhaust: High-temperature gases discharged from the rotary kiln come into contact with the material, transferring heat to it.
Gradual temperature rise: After passing through multiple preheating stages, the material’s temperature steadily increases before it enters the rotary kiln for calcination.
Reducing heat waste: Heat from the exhaust gas—which might otherwise be vented directly—is recovered and reused, helping to lower fuel consumption.
Take a lime production line, for example: when limestone is preheated before entering the rotary kiln, it reaches the required calcination temperature faster, thereby reducing the thermal load on the kiln.
In short, the preheater “primes” the material with heat beforehand, allowing the rotary kiln to use less fuel and focus its thermal energy where it is truly needed for calcination.
Preheater Optimization Checklist
Parameter
Potential Issue
Recommended Check
Material particle size
Uneven heating
Check particle size distribution
Material moisture content
Increased thermal load
Check raw material moisture
Flue gas temperature
Insufficient heat recovery
Check airflow and heat exchange
Airflow distribution
Localized under-heating
Check airflow balance
Pressure drop
Ash accumulation, blockage
Monitor pressure drop trends
Residence time
Insufficient heat exchange
Check feed rate and equipment load
The ultimate goal is not simply to pursue higher preheater outlet temperatures, but rather to achieve a stable feed condition for the kiln using less energy, while ensuring process requirements are met.
How does a rotary kiln cooler work?
A rotary kiln cooler cools down the high-temperature material discharged from the rotary kiln while simultaneously recovering and utilizing as much of the heat as possible.
Its working principle is actually quite simple:
High-temperature material enters the cooler: Upon exiting the rotary kiln, the material is still at a high temperature and requires further cooling.
Temperature reduction via air or other media: Cold air exchanges heat with the hot material, carrying away the heat.
Heat recovery: The heated air—having absorbed the heat—can be fed back into the kiln or other heating equipment for reuse, provided the process allows for it.
Discharge of cooled material: After cooling, the material’s temperature drops to a level suitable for transport, storage, or subsequent processing.
Different types of coolers operate in different ways. For instance, rotary coolers rely on the rotation of the shell to continuously tumble the material and facilitate heat exchange, whereas grate coolers primarily use cold air passing through a bed of clinker to achieve cooling.
In short, the cooler does more than just lower the material’s temperature; its crucial role is to maximize heat utilization, minimize energy waste, and help the production line reduce operating costs.
How do preheaters and coolers affect thermal efficiency?
The key to how preheaters and coolers influence thermal efficiency lies in their ability to effectively utilize heat and minimize waste.
Preheaters: Maximizing the use of heat from exhaust gases
Flue gas discharged from a rotary kiln carries high heat; if vented directly, that energy is wasted.
Preheaters capture this high-temperature flue gas to pre-heat the raw materials, bringing them to a specific temperature before they enter the rotary kiln. This reduces the fuel required by the kiln, thereby increasing overall thermal efficiency.
Coolers: Recovering heat from high-temperature products
After calcination, the product remains at a high temperature. Direct cooling would result in a loss of heat.
Coolers lower the product’s temperature by transferring its heat to the cooling air; this heated air is then fed back into the kiln or other heating stages, reducing the need for additional fuel.
In short, the preheater determines how much heat is utilized from exhaust gases, while the cooler determines how much heat is recovered from the hot product. The better these two components work together, the more energy-efficient the production line generally becomes.
Why are refractory materials linked to thermal efficiency?
Refractory materials influence the thermal efficiency of rotary kilns primarily by minimizing heat loss while maintaining a stable internal temperature.
Reducing heat loss: Materials with superior thermal insulation properties generally reduce heat dissipation from the kiln shell, leading to lower fuel consumption.
Stabilizing calcination temperatures: Appropriate refractory materials help maintain a consistent operating temperature within the kiln, ensuring more uniform material calcination.
Reducing downtime for maintenance: Refractories with high heat and wear resistance offer a longer service life, thereby minimizing losses associated with kiln shutdowns for repairs.
In short, refractory materials do more than just protect the kiln structure; they are crucial for heat retention and the stability of production operations.
How can preheater and cooler performance be optimized?
In rotary kiln production, preheaters and coolers directly impact heat utilization, fuel consumption, and production stability. Improving equipment performance requires a holistic approach that goes beyond temperature control; it involves optimizing airflow, material flow, equipment structure, and daily maintenance. Simply put, the goal is to achieve more thorough preheating, more uniform cooling, and more effective heat recovery.
1. Preheater Performance Optimization
The primary function of a preheater is to utilize high-temperature exhaust gas discharged from the rotary kiln to preheat the feed material, thereby reducing the thermal load inside the kiln. Poor preheating performance leads to increased heat loss via exhaust gases and potentially higher fuel consumption. Optimization efforts should focus on the following areas:
Enhance gas-solid heat exchange efficiency: Optimize airflow distribution to ensure full contact between the material and the high-temperature gas, minimizing issues caused by inadequate heat exchange.
Minimize air leakage: Inspect equipment connections, access doors, and sealing points to prevent cold air from entering the system, which would lower exhaust gas temperatures and increase the system’s thermal load.
Prevent blockages and material buildup: Regularly inspect discharge pipes, cyclone separators, and areas prone to accumulation to ensure smooth material flow and maintain preheating effectiveness.
Control material feed rates: Maintain a stable feed rate; avoid overloading or excessive fluctuations that could disrupt gas-solid heat exchange and system operation.
Strengthen temperature and pressure monitoring: Monitor temperatures, pressure differentials, and exhaust gas temperatures across all preheater stages to promptly detect issues such as blockages, air leaks, or reduced heat exchange efficiency.
2. Cooler Performance Optimization
The primary function of the cooler is to lower the temperature of the product discharged from the kiln while recovering as much of the heat carried by the product as possible. Poor cooling performance not only affects downstream conveying and processing but can also result in heat loss. Optimization efforts can focus on the following areas:
Properly control cooling airflow: Adjust airflow based on material temperature and production output to ensure effective cooling while avoiding unnecessary fan energy consumption.
Improve material distribution: Ensure the material passes through the cooling zone as evenly as possible to prevent localized accumulation or excessive bed thickness, which can lead to uneven cooling.
Increase heat recovery rates: Where the process permits, redirect high-temperature cooling air back to the rotary kiln or other heating stages for reuse.
Check for equipment wear and air leakage: Regularly inspect seals, grate plates, drive components, and high-wear areas to minimize air leakage and unplanned downtime.
Monitor discharge temperature: Control the discharge temperature to meet downstream conveying, storage, or processing requirements, while also monitoring the temperature and flow rate of the recovered hot air.
3. Comparison of Key Optimization Points for Preheaters and Coolers
Optimization Areas
Preheater
Cooler
Core Objectives
Enhance material preheating efficiency
Lower product temperature and recover heat
Airflow Optimization
Improve airflow distribution; reduce air leakage
Optimize cooling air volume and pressure
Material Management
Maintain stable feeding; minimize blockages
Improve material bed distribution; prevent localized accumulation
Equipment Maintenance
Inspect for build-up (crusting), blockages, and seal integrity
Check for wear, seal condition, and drive components
Key Monitoring Points
Temperatures at various stages, pressure differentials, exhaust gas temperature
Discharge temperature, hot air temperature, air volume
Energy Conservation Focus
Reduce heat loss via exhaust gas
Increase product waste heat recovery rate
For equipment operation, neither higher temperatures nor greater airflow rates are necessarily better. Optimization of the preheater focuses on enhancing heat exchange efficiency and minimizing air leakage and blockages, whereas optimization of the cooler focuses on improving cooling performance and increasing the waste heat recovery rate. Only through their coordinated operation can energy consumption be effectively reduced and the overall thermal efficiency of the rotary kiln production line improved.
Common Operational Issues and Troubleshooting Methods
The following issues can serve as a starting point for equipment diagnosis; however, a specific symptom does not necessarily correspond to a specific fault.
Symptom
Possible Cause
Items to Check
Recommendation
High flue gas temperature at preheater outlet
Insufficient heat exchange, excessive flue gas volume, high material moisture, air leakage
Flue gas volume, moisture, temperature profile, seals
Identify primary source of heat loss
Continuous rise in preheater pressure drop
Dust accumulation, coating formation, blockage
Pressure differential trend, internal inspection
Clean and restore airflow
High cooler outlet temperature
Insufficient airflow, uneven material distribution, equipment wear
Airflow, material bed, equipment condition
Restore effective heat exchange
Low recovered air temperature
Insufficient heat exchange, air leakage, excessive airflow
What is the difference between a preheater and a cooler?
Although both involve heat recovery, their operational objectives are completely different.
Comparison Item
Rotary Kiln Preheater
Rotary Kiln Cooler
Location
Before the rotary kiln
After the rotary kiln
Material Handled
Raw materials entering the system
High-temperature calcined product
Primary Purpose
Increase feed temperature
Decrease product temperature
Heat Source
High-temperature process flue gas
High-temperature solid product
Heat Transfer Direction
Flue gas → Raw material
Product → Cooling air
Energy-Saving Effect
Reduces rotary kiln heating load
Recovers sensible heat from high-temperature product
Key Temperatures
Feed outlet, flue gas outlet
Product outlet, recovered air
Key Control Factors
Gas-solid heat exchange, pressure drop
Air volume, airflow distribution, bed characteristics
Common Issues
Insufficient heat exchange, high exhaust gas temperature
High discharge temperature, insufficient heat recovery
Key Refractory Issues
High temperature, erosion, dust accumulation, abrasion
Abrasion, thermal shock, mechanical impact
FAQ
Q: Is a higher preheater temperature always better?
A: No. Excessively high temperatures do not necessarily indicate optimal heat exchange; one must also consider exhaust gas temperature, material preheating effectiveness, and system heat loss. The key is to ensure efficient utilization of heat.
Q: Can the feed rate be continuously increased to improve preheating performance?
A: It is not recommended. An excessive feed rate can lead to inadequate heat exchange, increased pressure drop across the equipment, and even blockages. Feed rates should be reasonably controlled based on equipment capacity and actual operating conditions.
Q: Is simply clearing the blockage sufficient when a preheater becomes clogged?
A: Not necessarily. In addition to removing the blockage, one must investigate the root cause of the buildup—such as material properties, temperature fluctuations, or airflow conditions—to prevent the problem from recurring.
Q: What are the consequences of ignoring air leakage in the preheater?
A: Air leakage increases the volume of gas the system must handle, potentially raising fan load and negatively impacting preheating efficiency and fuel consumption. Therefore, checking for air leaks is crucial.
Q: Is a higher cooling airflow rate in the cooler always better?
A: No. Excessive airflow can increase fan power consumption without necessarily improving heat recovery. Airflow should be adjusted appropriately based on material temperature, production output, and hot air recovery requirements.
Q: Is it acceptable to focus solely on discharge temperature while ignoring waste heat recovery?
A: No, that is insufficient. The cooler must not only cool the product to the appropriate temperature but also recover as much heat as possible from the hot product; both aspects require consideration.
Q: What problems arise from uneven material distribution inside the cooler?
A: Material accumulation or uneven bed thickness can easily lead to localized cooling deficiencies and fluctuations in discharge temperature; it can also disrupt hot air distribution and impair heat recovery.
Q: Is periodic maintenance unnecessary as long as the equipment is still running?
A: No. Wear on components such as seals, grate plates, and drive mechanisms can gradually degrade equipment performance. Regular inspections help identify issues early and reduce unplanned downtime.
Q: Is looking solely at fuel consumption sufficient when optimizing preheaters and coolers?
A: No. Attention must also be paid to fan power consumption, system pressure drop, material throughput, product quality, and operational stability to avoid a scenario where fuel consumption decreases while other operating costs rise.
Q: Can preheaters and coolers be optimized separately?
A: They can be examined individually, but it is best to evaluate them in the context of the entire production line. The preheater affects the material temperature before it enters the rotary kiln, while the cooler impacts waste heat recovery; effective coordination between the two is essential for maximizing overall energy efficiency.
Summary
Rotary kiln preheaters and coolers are essential components for enhancing thermal efficiency, reducing energy consumption, and ensuring stable production operations. Properly configuring and optimizing these systems not only improves heat recovery efficiency but also lowers operating costs and extends equipment service life. Selecting the right equipment solution is key to achieving efficient and stable rotary kiln performance.
Whether you are planning a new rotary kiln production line or looking to optimize the operational efficiency of existing equipment, our expert team can provide tailored equipment selection and solutions based on your specific material characteristics, production capacity requirements, and process conditions.
Adjusting the flue gas control ratio of lime kiln rotary kiln (usually refers to the ratio of key components in the flue gas, such as O₂, CO, NOx, SO₂, etc.) needs to take into account the combustion efficiency, environmental protection requireme...
If you’re running a lime production line, you know the stress of flue gas control all too well. Mess up O₂, CO, NOx, or SO₂ levels, and you’re facing fines, shutdowns, or even damaged kiln equipment — not to mention wasted fuel and inconsistent l...
If you work in the mining, calcination, or mineral processing industry, you've likely encountered these problems: they are not only dirty and messy, but also consume enormous amounts of fuel, often failing to meet environmental standards. Chunl...
Sand is a fine-grained material of small minerals or rock fragments, mainly formed by rock weathering or mineral fragmentation, with grain sizes usually ranging from 0.0625 mm to 2 mm (according to the international standard ISO 14688). Sand can...
 Chunlei Rotary kiln